Catalog Showcase
Precision Surgical & Medical Power Tool Range
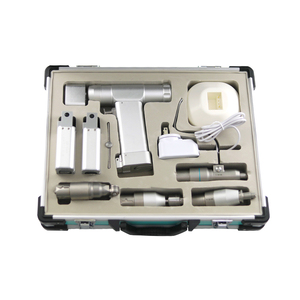
Hot Selling Animal Orthopedic Bone Surgical Medico Power Tool Mini Bone Drill Set Multi-functional Drill
Wholesale Hospital Equipment Orthopedic Surgical Power Tools for Trauma Surgery
Reusable Laparoscopic Single-lumen Puncture Needle 5*330mm 0.8mm Biliary Surgical Instrument
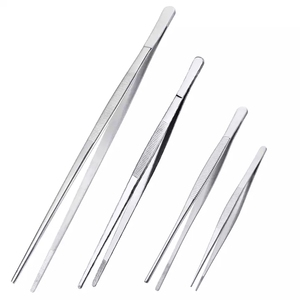
ZONWIN 12 Inch Stainless Steel Kitchen Chef Tweezers Sets Food Long Tong With Serrated Tips
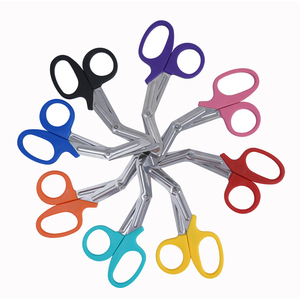
High Quality Stainless Steel First Aid Medical Bandage Scissors for Nurse
Medical Grade Autoclavable Dental Brush Bulk Surgical Scrub Brushes for Dental Clinics
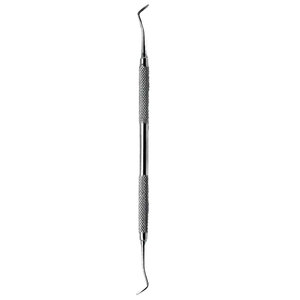
Medical High Quality Stainless Steel Double Ended Dental Explorer Probe Periodontal Diagnostic Tool
Production Excellence at a Glance
Factory Benchmarks & Export Metrics
>500,000
Annual Surgical Units
99.85%
First-Pass QA Rate
65+
Countries Exported
±0.005mm
CNC Swiss Tolerances
1. Metallurgical Science & Precision Manufacturing Standards in Spinal Instrumentation
Modern spinal surgery demands an uncompromised convergence of materials science, biomechanical engineering, and microscopic dimensional control. As a premier China spine surgical instruments factory and global exporter, our manufacturing floor operates at the intersection of clinical utility and industrial rigor. Spinal implants and surgical instruments—ranging from cervical pedicle screw drivers to lumbar micro-Kerrison rongeurs—operate within harsh biochemical environments and are subjected to severe multi-axial fatigue stress, high torsional torque, and aggressive repeated steam autoclave sterilization protocols.
Information Gain Insight: The mechanical failure of spinal instruments during surgery is rarely caused by static overload; it stems from micro-fretting corrosion, stress concentration at machining tool marks, or inadequate heat-treatment phase transformation. Our factory eliminates these failure modes by implementing vacuum double-tempering processes and automated ultrasonic electropolishing.
To guarantee long-term clinical safety, material selection is dictated by the specific mechanical requirement of the surgical task. We primarily employ medical-grade titanium alloy Ti-6Al-4V ELI (ASTM F136 / ISO 5832-3) and martensitic surgical stainless steels (AISI 420, AISI 440A, AISI 630 / 17-4PH). Below is an engineering comparison of the raw metals utilized in our spine instrument manufacturing process:
| Material Grade | Standard Specification | Tensile Yield Strength (MPa) | Hardness (HRC) | Primary Clinical Application |
|---|---|---|---|---|
| Ti-6Al-4V ELI | ASTM F136 / ISO 5832-3 | ≥ 795 MPa | 30 - 35 HRC | Spinal Rod Extensions, MISS Dilators, Polyaxial Screw Drivers |
| AISI 17-4PH (Custom 630) | ASTM F899 / ISO 7153-1 | ≥ 1100 MPa | 40 - 45 HRC | High-Torque Rod Benders, Counter-Torque Drivers, Shaft Retractors |
| AISI 420 (High Charpy Value) | ASTM F899 / EN 1.4021 | ≥ 800 MPa | 50 - 54 HRC | Kerrison Rongeur Blades, Bone Chisels, Curette Cutting Tips |
| PEEK Optima & Carbon Fiber | ASTM F2026 | ≥ 170 MPa | Rockwell R126 | Radiolucent Retractor Blades & Interbody Trial Handles |
Surface Passivation and Corrosion Mitigation Protocols
All stainless steel spine instruments manufactured in our facility undergo rigorous citric acid or nitric acid passivation in strict accordance with ASTM A967 and ISO 16061. Passivation selectively dissolves free iron from the surface of the instrument, forming a continuous, self-healing chromium oxide ($\text{Cr}_2\text{O}_3$) passive layer. This critical step ensures that instruments withstand thousands of cleaning cycles using enzymatic detergents and high-temperature steam autoclaving ($134^\circ\text{C}$ at $2.1\text{ bar}$) without suffering from pitting, crevice corrosion, or stress-corrosion cracking (SCC).
2. Comprehensive Spine Surgery Instrument Portfolio & System Solutions
Spinal pathologies—including degenerative disc disease, scoliosis deformities, spinal stenosis, and traumatic fractures—require specialized instrument architectures. Our OEM/ODM production lines manufacture complete instrument sets optimized for specific anatomical approaches: Anterior Cervical Discectomy and Fusion (ACDF), Posterior Lumbar Interbody Fusion (PLIF), Transforaminal Lumbar Interbody Fusion (TLIF), Extreme Lateral Interbody Fusion (XLIF), and Minimally Invasive Spine Surgery (MISS).
Pedicle Screw Fixation Instrumentation
Complete tooling for occipitocervical, thoracolumbar, and sacral fixation. Includes monoaxial/polyaxial pedicle screw drivers with quick-connect silicone handles, self-tapping bone taps, pedicle probes (Lenke curve and straight), ball-tip feelers, and friction-controlled rod benders.
MISS Tubular Retractor Systems
Engineered for microdiscectomy and MIS-TLIF. Features expandable carbon-fiber or titanium tubular retractors with integrated cold-light fiber optic illumination channels, progressive sequential muscle dilators ($14\text{mm}$ to $26\text{mm}$ outer diameter), and multi-angle flexible articulated arms.
Decompression & Bone Resection Set
High-precision bone removal tools. Includes ultra-smooth ejector Kerrison Rongeurs ($1\text{mm}$ to $6\text{mm}$ bite sizes, $40^\circ$ and $90^\circ$ up/down biting), pituitary forceps, osteotomes, Cobb elevators, and angled endplate preparation curettes with ergonomic PEEK handles.
Sub-Micron Machining Quality Control for Kerrison Rongeurs
The Kerrison Rongeur is widely considered the ultimate test of a surgical instrument manufacturer's mechanical skill. A clearance gap of greater than $0.015\text{mm}$ between the sliding footplate and the main body will result in tissue tearing rather than clean bone cutting. Our factory utilizes 5-axis Wire Electrical Discharge Machining (WEDM) to maintain a sliding clearance of $0.008\text{mm} \pm 0.002\text{mm}$. Furthermore, the cutting tips are coated with Physical Vapor Deposition (PVD) Titanium Nitride (TiN) or Diamond-Like Carbon (DLC) to increase surface hardness to over $70\text{ HRC}$, reducing re-sharpening frequency by $400\%$.
3. Global Procurement Trends & Technological Innovations (2025–2030)
The global spinal surgery device market is undergoing a structural transition driven by cost-containment pressures, stringent regulatory regimes (such as the European Union’s EU MDR 2017/745 and US FDA 510k modernization mandates), and the rapid clinical adoption of robotic-assisted spine surgery and intraoperative navigation systems. Medical device brands, hospital group purchasing organizations (GPOs), and regional distributors must realign their procurement strategies to capture competitive advantage.
Key Strategic Shifts in Spine Instrument Sourcing:
- Robotic & Navigation-Ready Tooling: Traditional manual instruments are being upgraded with dynamic optical or electromagnetic navigation array mounts. Instruments produced in our factory feature integrated passive reflective marker posts calibrated to sub-millimeter concentricity ($\le 0.05\text{mm}$ runout) for direct compatibility with Medtronic StealthStation, Brainlab, and Globus ExcelsiusGPS platforms.
- 3D Printed Porous Implants & Specialized Insertion Tooling: As additive manufacturing (Selective Laser Melting / SLM) dominates the production of titanium interbody cages, traditional impaction tools are evolving. New insertion instruments require low-friction quick-release mechanisms that protect delicate 3D-printed porous lattices during high-impact malleting.
- Carbon-PEEK Radiolucent Retractor Systems: Metal artifacts under intraoperative X-ray and C-arm fluoroscopy compromise surgical accuracy. Sourcing trends show a $28\%$ compound annual growth rate (CAGR) in non-metallic, radiolucent PEEK retractor systems that allow unobstructed 3D fluoroscopic visualization during MISS procedures.
- Single-Use Sterile Kits vs. High-Durability Modular Trays: While outpatient Ambulatory Surgery Centers (ASCs) favor pre-sterilized single-use spinal discectomy kits, tertiary academic medical centers are doubling down on ultra-durable, fully dismantlable modular instrument systems designed for 1,000+ autoclave cycles to minimize environmental footprint and per-procedure cost.
4. Factory Infrastructure, Quality Management & OEM/ODM Enterprise Advantages
As a leading Chinese surgical instrument manufacturer and global exporter, our state-of-the-art facility integrates European precision machinery with continuous ISO 13485 certified quality management systems. We bridge the gap between low-cost sourcing and high-tier medical device engineering, offering international partners an end-to-end manufacturing footprint.
Our Core Enterprise Capabilities & Infrastructure
5-Axis CNC Swiss Machining
Equipped with DMG MORI and Citizen Swiss-type multi-axis lathes, enabling single-pass production of intricate pedicle screw components, complex handle splines, and cannulated shafts up to $450\text{mm}$ in length.
100% CMM & Optical Metrology
Every batch of critical spinal instruments undergoes automated dimensional verification using Zeiss Coordinate Measuring Machines (CMM) and Keyence 3D optical profilometers to ensure total blueprint compliance.
Class 10,000 Cleanroom Packaging
For pre-sterilized OEM products, our facility houses an ISO Class 7 (Class 10,000) cleanroom dedicated to ultrasonic cleaning, medical-grade Tyvek heat-sealing, and bioburden testing.
Full Traceability & UDI Laser Marking
Complete lot and batch traceability from raw material mill test reports (MTR) to final packaging. Automated fiber-laser marking for Unique Device Identification (UDI) matrix codes compliant with US FDA and EU MDR rules.
Distributor & OEM Support: We support custom tray layout design, laser logo branding, custom anodization color-coding for size identification, and complete technical file documentation (STED format) to accelerate your market authorization and registration processes in destination countries.
5. Frequently Asked Questions (FAQ) for Importers & Medical Device Procurement
Below are authoritative technical answers to the most common questions raised by biomedical procurement officers, orthopedic distributors, and hospital purchasing committees during factory supplier audits.
Our manufacturing facilities operate in full compliance with ISO 13485:2016 (Medical Devices - Quality Management Systems) and ISO 9001:2015. Our product catalogue is CE marked according to the European Medical Device Regulation (EU MDR 2017/745). For North American clients, our production processes align with US FDA Quality System Regulation (QSR 21 CFR Part 820), and technical files are maintained for 510(k) reference on OEM/ODM projects.
For standard catalogue instruments (such as standard Kerrison rongeurs, Cobb elevators, or pedicle probes), our baseline MOQ starts at 20 pieces per item. For full custom OEM/ODM projects involving custom forge dies, unique silicone handles, or proprietary retractor geometries, the initial prototyping MOQ starts at 50 to 100 units depending on component complexity and material raw stock requirements.
Raw metal materials are procured exclusively from certified medical-grade steel mills with accompanying Mill Test Certificates (MTC) detailing chemical composition and mechanical properties. Stainless steel and titanium raw stocks are strictly isolated in dedicated storage facilities. We conduct X-ray Fluorescence (XRF) spectrographic analysis on incoming raw material bars to verify chemical composition before any machining commences.
Yes. We offer high-resolution fiber laser marking for corporate logos, part numbers, lot codes, and GS1-compliant 2D DataMatrix UDI codes. Furthermore, we design custom anodized aluminum sterilization trays with engineered silicone insert blocks tailored specifically to your instrument set layout, ensuring optimal positioning during transport and autoclaving.
Standard catalog orders are dispatched within 15 to 25 business days. Custom OEM orders requiring new tooling and pre-production sample approval generally take 30 to 45 business days. We export under all major Incoterms (EXW, FOB, CIF, DDP) via international express couriers (DHL, FedEx, UPS), air freight for urgent clinical requirements, or ocean freight for high-volume bulk packaging.